Introduction
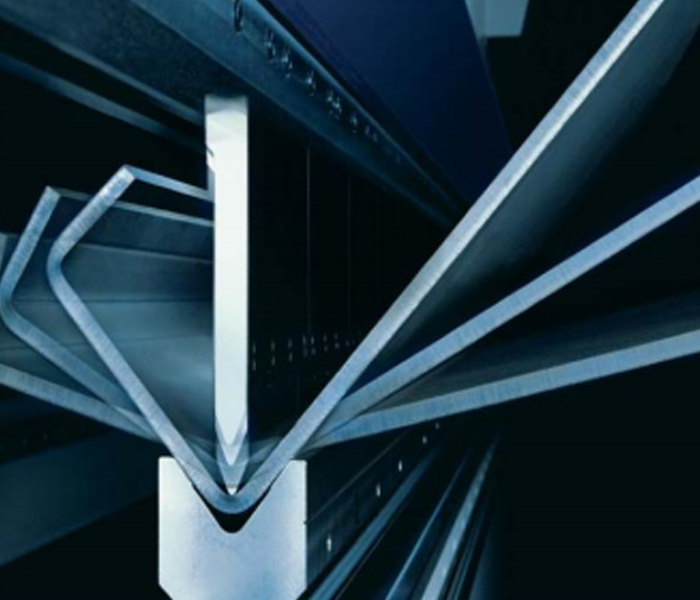
Air bending and bottom bending are two common methods used in press brake sheet metal fabrication.
Both processes use a punch and die to form sheet metal, but they differ in how the material interacts with the tooling.
Understanding this difference is important when selecting a press brake, choosing tooling, calculating bending force, or deciding which production method is most appropriate for a particular application.
For many modern sheet metal manufacturers, air bending offers greater flexibility and is widely used on CNC press brakes. Bottom bending, however, still has important applications where specific requirements justify the additional force and tooling considerations.
What Is Air Bending?
In air bending, the sheet is positioned over a V-shaped lower die.
The punch moves downward and pushes the sheet into the die opening without forcing the entire sheet surface into contact with the bottom of the die.
The final angle is primarily controlled by the depth of punch penetration.
For example, a machine may use the same basic tooling to produce several different angles by changing the programmed ram position.
This flexibility is one of the major advantages of air bending.
What Is Bottom Bending?
In bottom bending, the punch pushes the sheet further into the die until the material comes into contact with the bottom area of the die.
The tooling geometry therefore has a stronger influence on the final bend angle.
Because the material is pressed more firmly against the die, bottom bending generally requires more force than air bending.
It can provide good repeatability when the correct tooling and process parameters are used.
The Key Difference
The simplest way to understand the difference is:
Air bending controls the angle primarily through punch penetration.
Bottom bending relies more heavily on the geometry of the tooling and the material being formed against the die.
This difference affects flexibility, force requirements, tooling selection, and production strategy.
Air Bending: Main Advantages
Greater Flexibility
One of the biggest advantages of air bending is its flexibility.
A single die opening can often be used to produce different bend angles by adjusting the ram position.
This is particularly valuable for job shops and manufacturers producing many different components.
Lower Force Requirements
Air bending generally requires less force than bottom bending for comparable applications.
This can allow manufacturers to process certain parts using a machine with lower nominal tonnage.
Flexible Tooling
Because the final angle is controlled largely through machine position, the same tooling setup can support a range of bending angles.
This can reduce tooling changes.
Suitable for CNC Production
Air bending works well with CNC press brakes because the bending angle can be controlled through precise ram positioning.
This makes it particularly suitable for modern programmable production.
Bottom Bending: Main Advantages
Good Repeatability
When the tooling, material, and process are properly controlled, bottom bending can provide consistent results.
Specific Angle Requirements
For certain production applications, bottom bending can be advantageous when a consistent angle is required repeatedly.
Reduced Springback in Some Applications
The additional forming force can reduce the effect of springback compared with a purely elastic deformation process, although actual results depend strongly on material and process conditions.
What Is Springback?
Springback is the tendency of sheet metal to partially return toward its original shape after the bending force is removed.
It occurs because the material experiences both plastic and elastic deformation during bending.
Springback can vary depending on:
- Material type
- Material strength
- Thickness
- Bend radius
- Bending method
- Tooling
- Grain direction
A machine may therefore require angle compensation to achieve the desired final geometry.
Modern CNC systems can help operators manage this variation through programmed compensation and, on advanced machines, automatic angle measurement.
Which Method Is More Accurate?
There is no universal answer.
Accuracy depends on the complete process rather than simply choosing air bending or bottom bending.
Important factors include:
- Machine rigidity
- Tooling accuracy
- Material consistency
- Machine positioning
- Operator skill
- Backgauge accuracy
- Compensation technology
- Process control
A well-configured CNC press brake using air bending can achieve very high levels of repeatability.
Similarly, bottom bending can deliver excellent consistency when the application is properly controlled.
Which Method Is More Flexible?
Air bending generally offers greater flexibility.
Because the angle can be changed through ram position, manufacturers can produce different angles without necessarily changing the tooling.
This makes air bending particularly attractive for:
- Job shops
- Prototype production
- High-mix manufacturing
- Low-volume production
- Custom sheet metal fabrication
Bottom bending is often more attractive when the production process is highly standardized.
How Does Tooling Affect the Process?
Tooling is critical for both methods.
The die opening affects the bending process, while punch geometry influences the internal bend radius and material deformation.
Tool condition also matters.
Damaged, worn, or poorly manufactured tooling can contribute to:
- Angle variation
- Surface marking
- Dimensional inconsistency
- Setup problems
For professional sheet metal manufacturers, tooling should therefore be considered an integral part of the bending process.
Which Method Requires More Tonnage?
As a general rule, bottom bending requires more force than air bending.
However, exact force requirements depend on material, thickness, bending length, die geometry, and other process variables.
Machine buyers should never determine press brake capacity based only on a general rule.
The required tonnage should be calculated for the actual production application.
Which Method Should You Choose?
Choose Air Bending When:
- You need flexibility
- You produce many different parts
- You work with different bending angles
- You want to minimize tooling changes
- You operate a CNC press brake
- You have mixed production requirements
Consider Bottom Bending When:
- You produce large quantities of similar parts
- Specific tooling geometry is advantageous
- Repeatable fixed angles are important
- The additional forming force is acceptable
- The process is highly standardized
In many modern sheet metal factories, air bending is the preferred general-purpose method because it provides a strong combination of flexibility, efficiency, and CNC compatibility.
A Practical Example
Consider a manufacturer producing electrical cabinet components.
The production may involve 90°, 45°, and other angles across different parts.
With air bending, the manufacturer may be able to use compatible tooling and change the programmed ram position to achieve different angles.
Now consider a manufacturer producing thousands of identical structural components with a standardized bending process.
Bottom bending may become attractive if its tooling and process characteristics provide a suitable combination of consistency and productivity.
The correct choice depends on production economics rather than simply which method is technologically newer.
Final Thoughts
Air bending and bottom bending are not competing technologies where one is always superior.
They are different approaches to controlling sheet metal deformation.
Air bending provides flexibility and works particularly well with CNC press brake production. Bottom bending provides a more tooling-defined forming process and can be valuable for standardized applications.
For equipment buyers, the most important question is not “Which method is best?”
It is:
Which bending method best matches our materials, products, production volume, tooling strategy, and quality requirements?
KLD Machinery approaches press brake selection from this application perspective, helping customers evaluate machine configuration, tooling, control, and automation as one complete production system.
Frequently Asked Questions
Is air bending better than bottom bending?
Not always. Air bending is generally more flexible, while bottom bending can be advantageous for specific standardized applications.
Does air bending require less tonnage?
Generally yes, although actual requirements depend on material, thickness, bending length, tooling, and other factors.
Can air bending produce accurate parts?
Yes. Modern CNC press brakes can achieve highly repeatable results with properly selected tooling, machine configuration, and process control.
Does bottom bending eliminate springback?
No. It can reduce springback effects in some applications, but material characteristics and process conditions still influence the final result.